

Technical Specifications
|
Parameter |
Details |
|
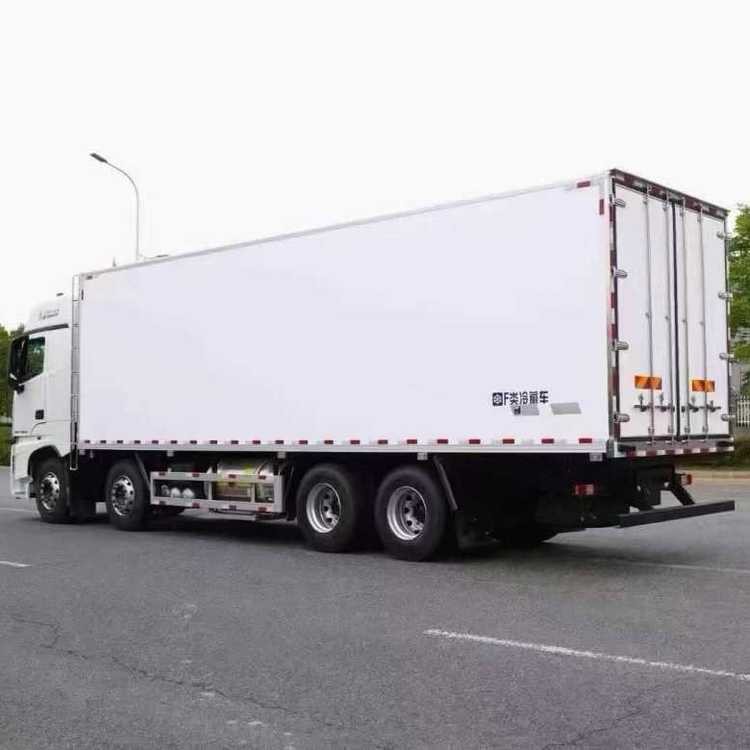
Overall Dimensions (L×W×H) |
12000-13750×2500-2550×3800-4200mm (customizable for regional regulations) |
|
Payload Capacity |
20-40 tons (varies by axle configuration, box size, and refrigeration unit) |
|
Box Volume |
70-110 cubic meters (depending on length and height) |
|
Temperature Range |
-30°C to +25°C (adjustable; precise control ±1°C) |
|
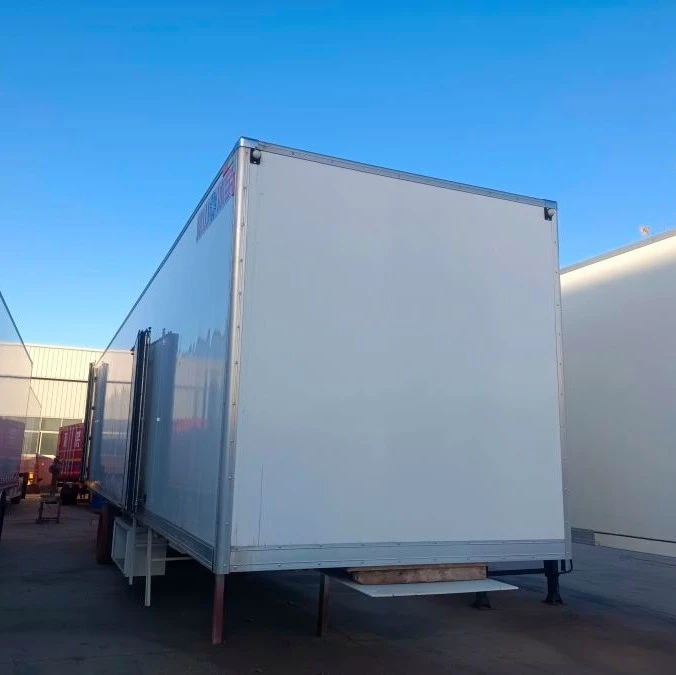
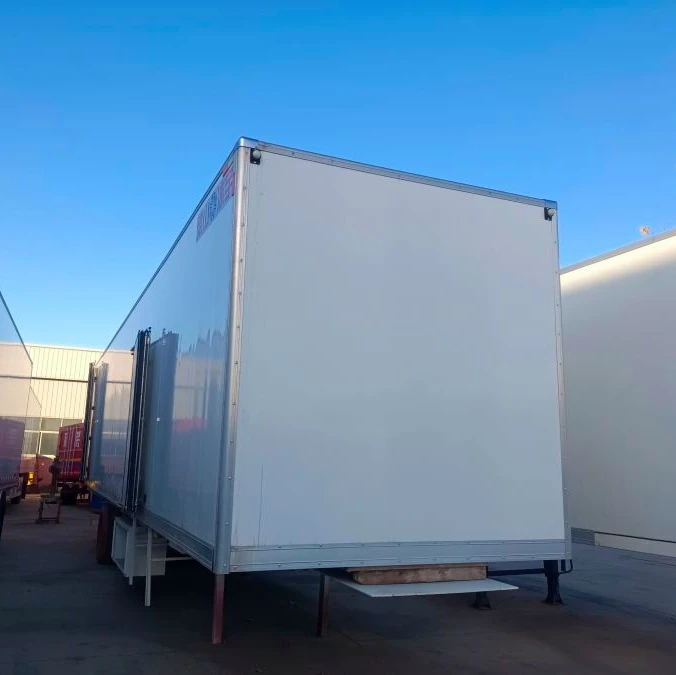
Box Structure |
Fully enclosed; High-density polyurethane (PU) foam insulation panels (80-120mm thickness); FRP/GRP inner/outer skins; Reinforced steel frame |
|
Refrigeration Unit |
Independent diesel-powered unit (Thermo King, Carrier, etc.); Electric standby mode (optional); Dual-circuit cooling system |
|
Axles |
2-4 heavy-duty axles (FUWA/BPW, 10-16 ton load per axle) |
|
Suspension System |
Air suspension (standard for cold chain); Mechanical leaf spring suspension (optional) |
|
Braking System |
WABCO dual-circuit pneumatic EBS with ABS anti-lock function & roll stability program (RSP) |
|
Door Configuration |
Rear double doors (full-width opening); Optional side door (1 set) for side loading; Air-tight rubber seals; Multi-point locking mechanism |
|
Flooring |
T-slotted aluminum floor or anti-slip composite floor; Drainage system (optional) |
|
Cargo Fixation |
8-16 reinforced lashing rings (load capacity: 5-10 tons each); Optional track-and-sliding lashing system |
|
Kingpin |
2.0/3.5 inch (JOST brand, ISO 1161 compliant) |
|
Tire Specification |
12R22.5 heavy-duty radial tires (4-8 tires based on axle count) |
|
Self-Weight |
9-12 tons (depending on box size and refrigeration unit) |
|
Optional Features |
GPS temperature monitoring, data logging, interior LED lights, ventilation system, air chute, partition wall, fuel heater, electric standby plug |
Core Advantages
Precise Temperature Control & Insulation: The high-density PU foam insulation panels (80-120mm thickness) provide exceptional thermal resistance, minimizing temperature fluctuations. The advanced refrigeration unit (Thermo King/Carrier) delivers rapid cooling/heating and maintains stable temperatures from -30°C to +25°C, ensuring compliance with cold chain standards for perishables and pharmaceuticals.
Superior Cargo Protection: The fully enclosed, air-tight box structure with sealed doors prevents temperature leakage, dust, moisture, and contamination. The corrosion-resistant FRP/GRP inner lining is easy to clean and sanitize, meeting food safety and pharmaceutical hygiene requirements.
Heavy-Duty & Durable Construction: High-tensile steel chassis and reinforced box frame ensure structural rigidity and load-bearing capacity, withstanding heavy loads and harsh road conditions. The air suspension (standard) provides smooth ride quality, reducing vibration and impact on sensitive cargo.
Enhanced Safety & Compliance: Equipped with WABCO's advanced EBS braking system, ABS, and RSP, the trailer ensures responsive, stable braking and minimizes rollover risks. It fully complies with ATP, CE, DOT, and CCC cold chain transport standards, facilitating cross-border perishable goods logistics.
Efficient Loading & Versatility: Rear double doors (full-width opening) and optional side door enable flexible loading/unloading via forklifts or pallet jacks. The T-slotted aluminum floor and lashing rings secure cargo during transit, while optional features like air chutes and partition walls optimize airflow and temperature uniformity.
Smart Monitoring & Energy Efficiency: Optional GPS temperature monitoring and data logging systems allow real-time tracking of temperature, location, and operating status, ensuring full cold chain visibility. The refrigeration unit's electric standby mode reduces fuel consumption and emissions during stationary loading/unloading.
Application Fields
Ideal for transporting temperature-sensitive cargo, including:
- Frozen goods: Frozen meat, seafood, poultry, ice cream, and frozen prepared foods (-18°C to -30°C).
- Chilled goods: Fresh fruits, vegetables, dairy products, eggs, flowers, and processed meats (0°C to +8°C).
- Pharmaceuticals: Vaccines, biologics, insulin, and temperature-sensitive medications (2°C to 8°C or controlled ambient).
- Other temperature-sensitive items: Chocolate, wine, chemicals, and electronic components.
Widely used in cold chain logistics, food distribution, pharmaceutical transport, agricultural exports, port transshipment, and long-haul cross-border transport, serving industries such as food processing, agriculture, pharmaceuticals, and retail.
Frequently Asked Questions (FAQ)
What is the temperature range of the refrigerated box semi-trailer?
Answer: It supports a wide temperature range from -30°C (deep freezing) to +25°C (heating/ambient control), with precise adjustment in 1°C increments to meet diverse cargo requirements.
How long can it maintain temperature without power?
Answer: With high-efficiency insulation, it can maintain stable temperatures for 4-8 hours (depending on external temperature and cargo) during short stops or power interruptions. The refrigeration unit's battery backup extends this period.
Is it compliant with international cold chain standards?
Answer: Yes, it fully complies with ATP (for perishable food), EU CE, US DOT, and Chinese CCC standards, making it suitable for global cross-border cold chain transport.
What refrigeration unit brands are available?
Answer: It is compatible with top-tier brands such as Thermo King and Carrier, ensuring reliable performance, global service networks, and easy access to spare parts.
Can it be customized for specific cargo?
Answer: Yes, customization options include box dimensions, insulation thickness, partition walls, air chutes, temperature monitoring systems, and electric standby to meet the unique needs of frozen, chilled, or pharmaceutical cargo.
What maintenance is required for the refrigeration system?
Answer: Regular maintenance includes checking refrigerant levels, cleaning condenser/evaporator coils, replacing air filters, inspecting electrical connections, and servicing the engine/generator every 500-1000 operating hours to ensure optimal cooling performance.
Is it compatible with standard tractors?
Answer: Yes, it fits most tractors equipped with ISO-standard 2.0/3.5 inch kingpin connections. For electric standby, a 380/400V power connection is required at loading docks
Hot Tags: refrigerated box semi-trailer, China refrigerated box semi-trailer manufacturers, suppliers, factory, Heavy duty Box Trailer, box semi trailer, Box type Semi trailer, Refrigerated Box Semi trailer, Side curtain Container Semi trailer


